Dense coating with a secure interface
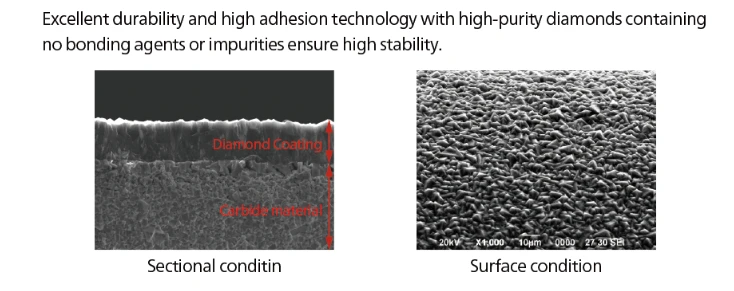
Substrate chemistry and microstructure promote diamond nucleation, reducing the risk of premature coating separation on the 3DEM series during abrasive cutting.
3DEM · Product family
Diamond coating · individual inspection · dimensional report available
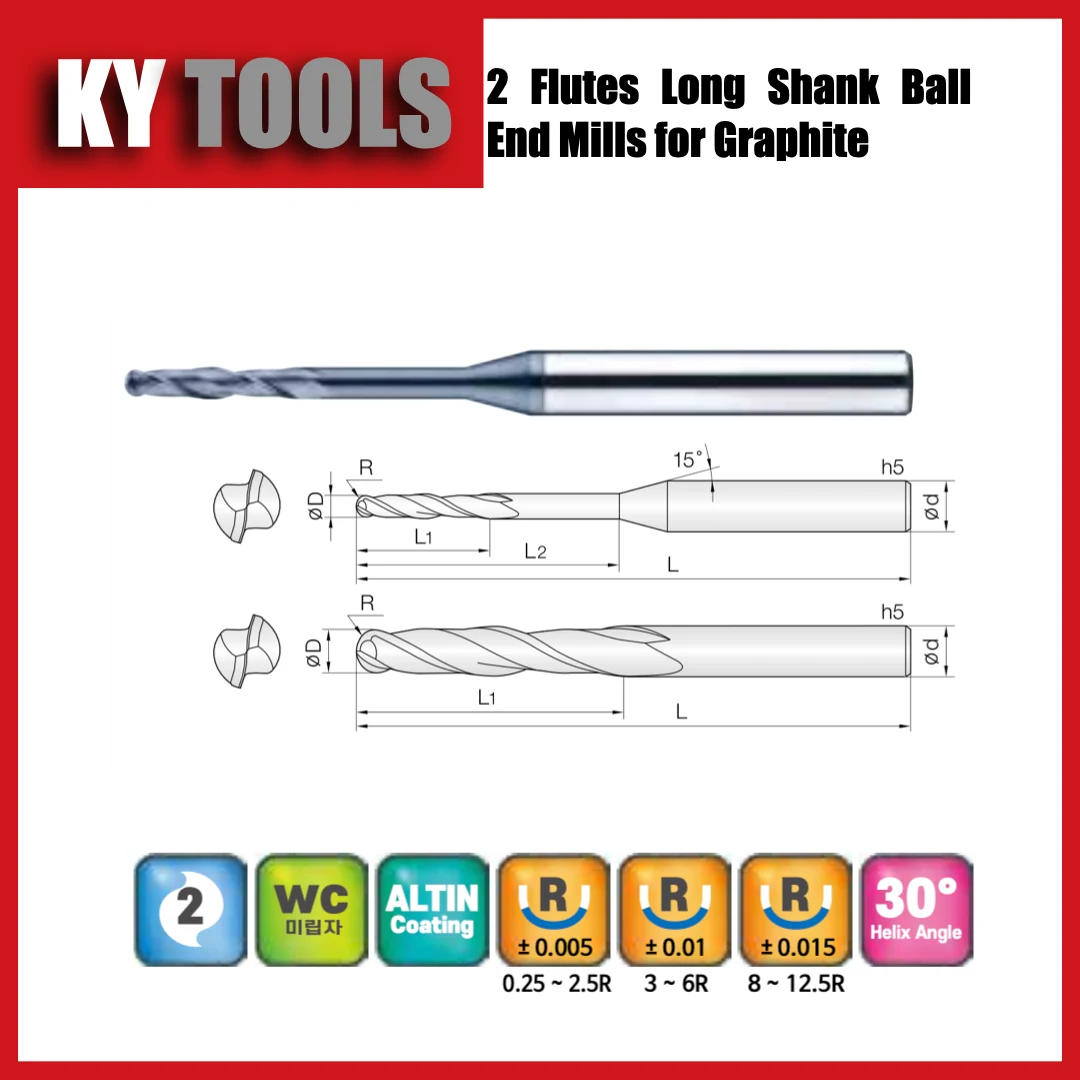
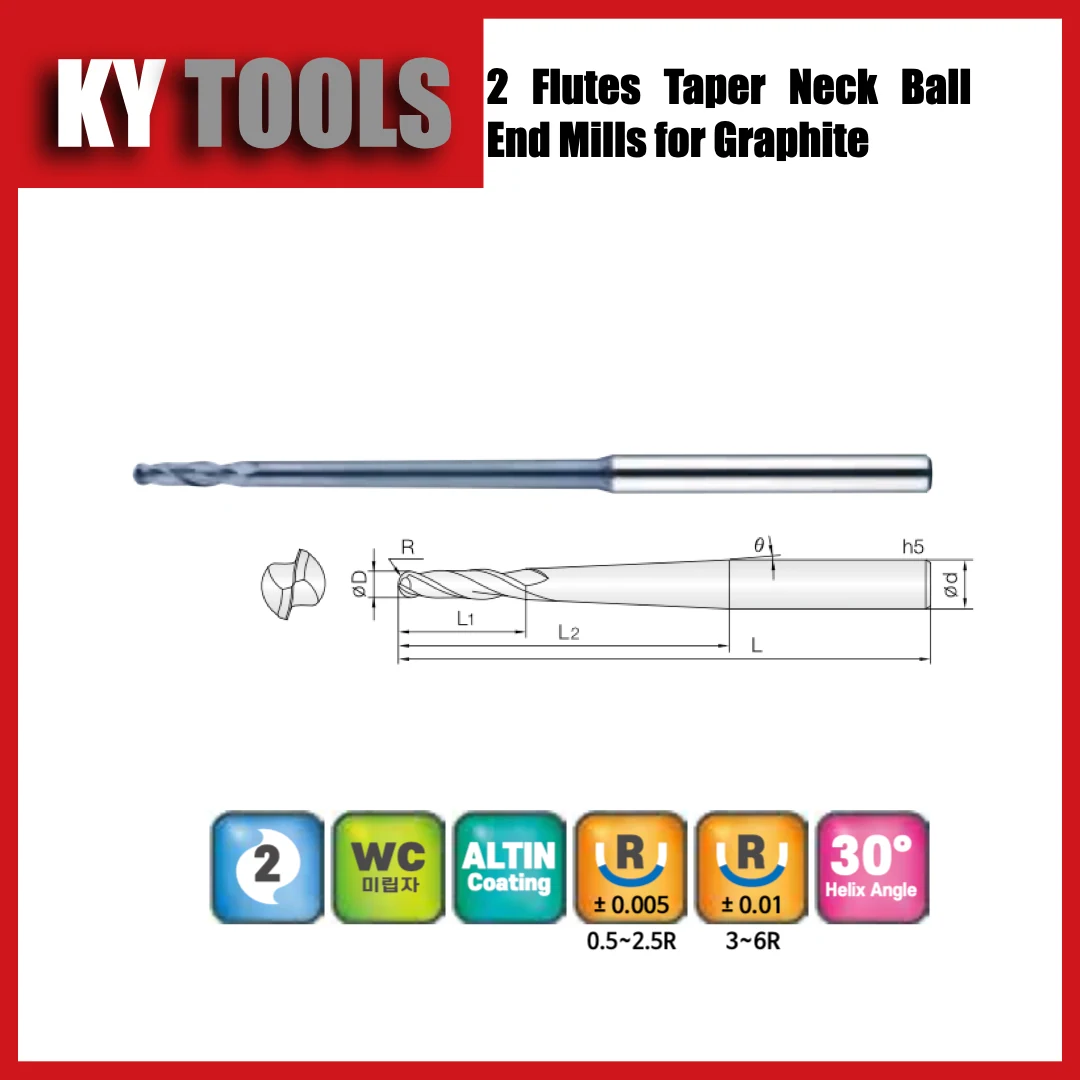
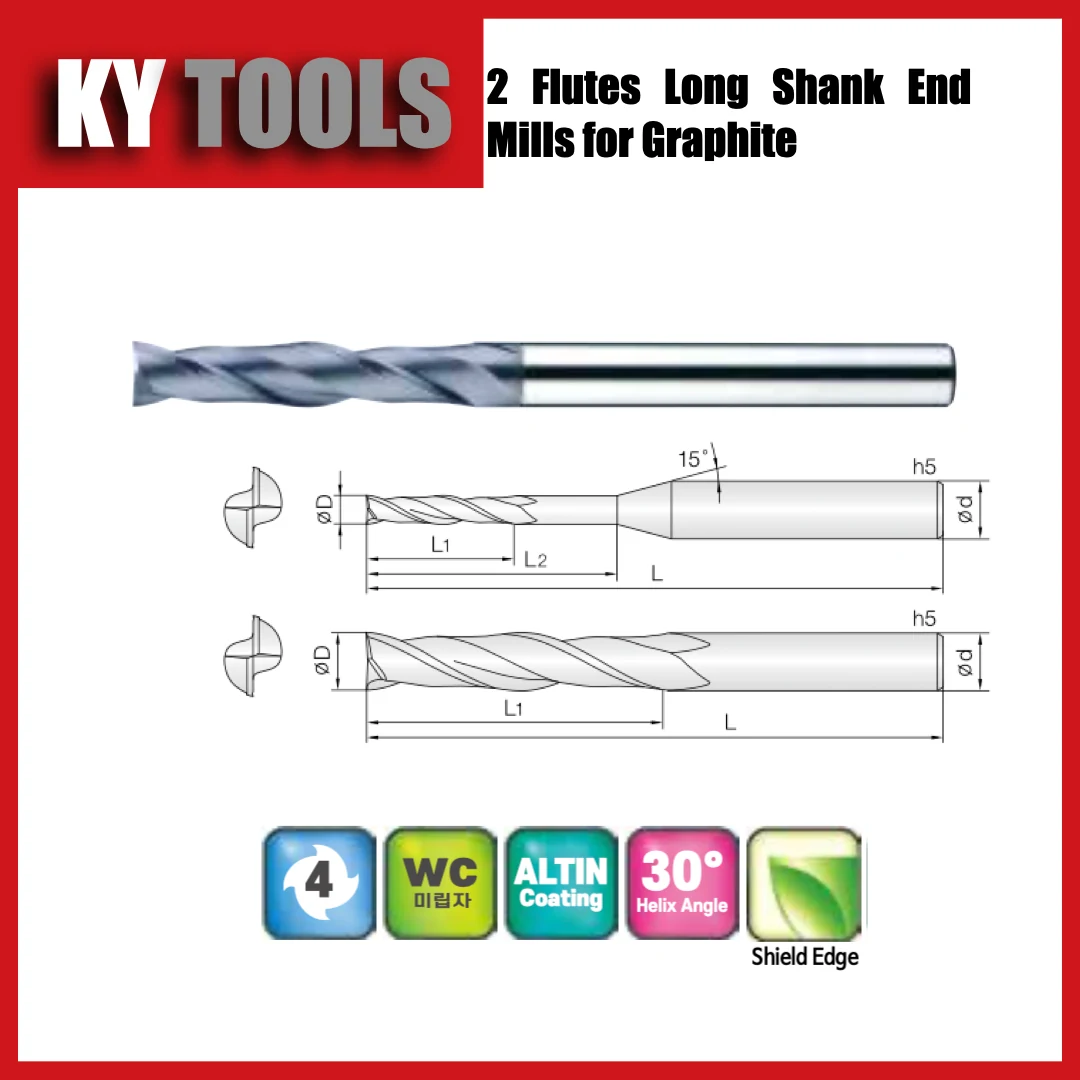
3 Flute Diamond Coated Square End Mills for Graphite currently shows Ø1–12 mm across 32 standard order codes. It combines a fine-grain carbide substrate selected for diamond-deposition compatibility with a square-end geometry for flat pocket floors, slots, shoulders, side walls, and edge milling. The standard-reach form keeps projection compact for rigid, repeatable production machining. Three flutes balance chip evacuation, core strength, and tooth engagement for general graphite profiling.
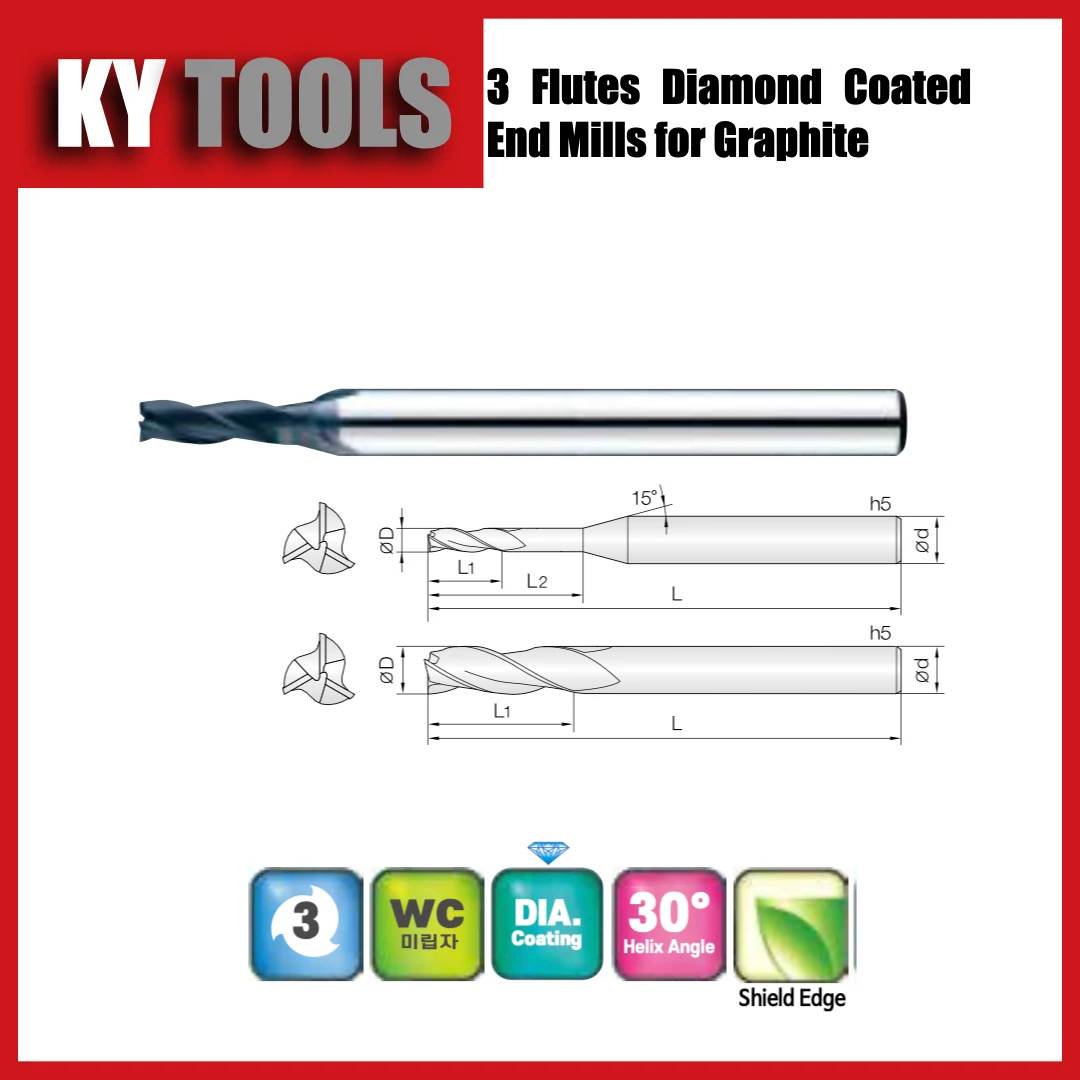
Standard series specifications
Select the end geometry, flute count, and reach style for the required profile, cutting depth, and chip evacuation. The size and price table below lists every standard order code, key dimension, and USD/pc reference price for engineering selection and purchasing.
3DEM coating and edge-retention evidence
Wear control at the peripheral edge and end teeth helps retain floor flatness, wall size, and a clean 90-degree feature transition. The standard-reach form keeps projection compact for rigid, repeatable production machining.
Substrate chemistry and microstructure promote diamond nucleation, reducing the risk of premature coating separation on the 3DEM series during abrasive cutting.
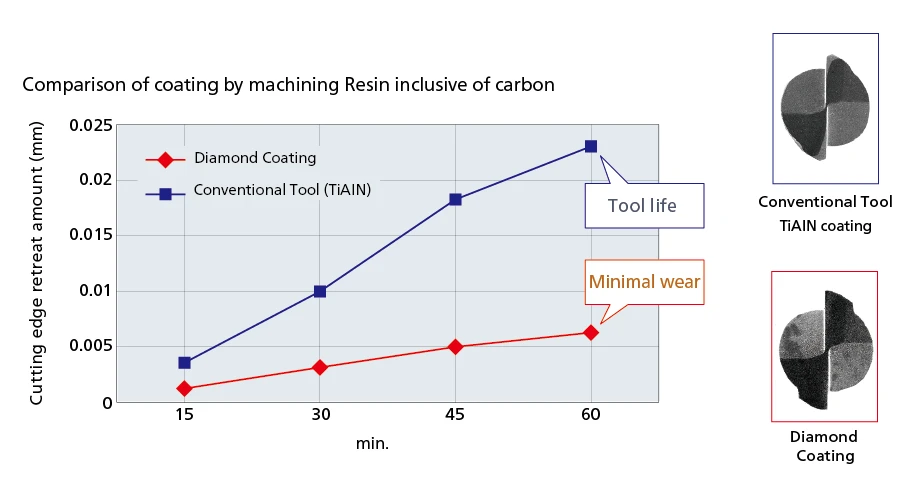
The shown carbon-resin test records about 0.006 mm edge retreat for diamond coating versus 0.023 mm for TiAlN. For this square-end geometry for flat pocket floors, slots, shoulders, side walls, and edge milling, lower wear supports more consistent profile retention.
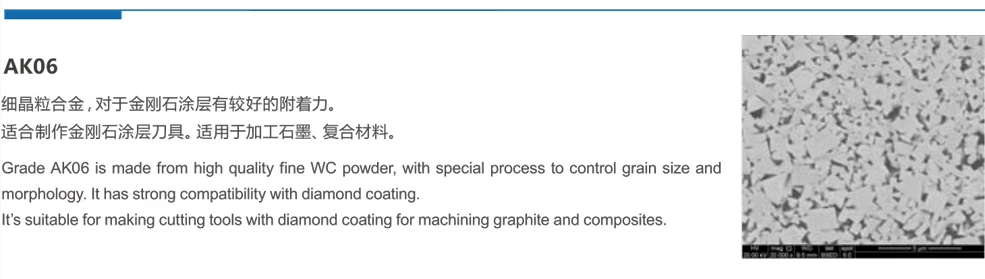
AK06 uses high-quality fine WC powder with controlled grain size and morphology, providing a diamond-compatible substrate for this 3-flute square end graphite end mill family.
Detailed codes, dimensions & reference prices
32 standard order codes with transparent online USD/pc FOB China prices updated 2026-Sep-14. Standard terms are 100% T/T in advance with a reference lead time of 10–15 working days. Final price and delivery are confirmed against quantity, dimensions, tolerance, and coating requirements.
Starting parameters for graphite
Choose cutter diameter, then select the applicable reach or taper combination to view spindle speed, feed rate, axial depth ap, and radial width ae. Use the result as a test-cut starting point and optimise for machine rigidity, actual overhang, runout, and graphite grade.
Send graphite grade, cutter diameter, actual overhang, maximum spindle speed, and roughing/finishing requirements so the starting parameters can be confirmed.
General-purpose graphite pocketing and profiling with balanced stability.
Extreme hardness also means brittleness. Use a rigid CNC, precision holder, and secure workholding; control runout especially on long-reach and small-diameter tools, and avoid impact entry.
3DEM dimensional verification
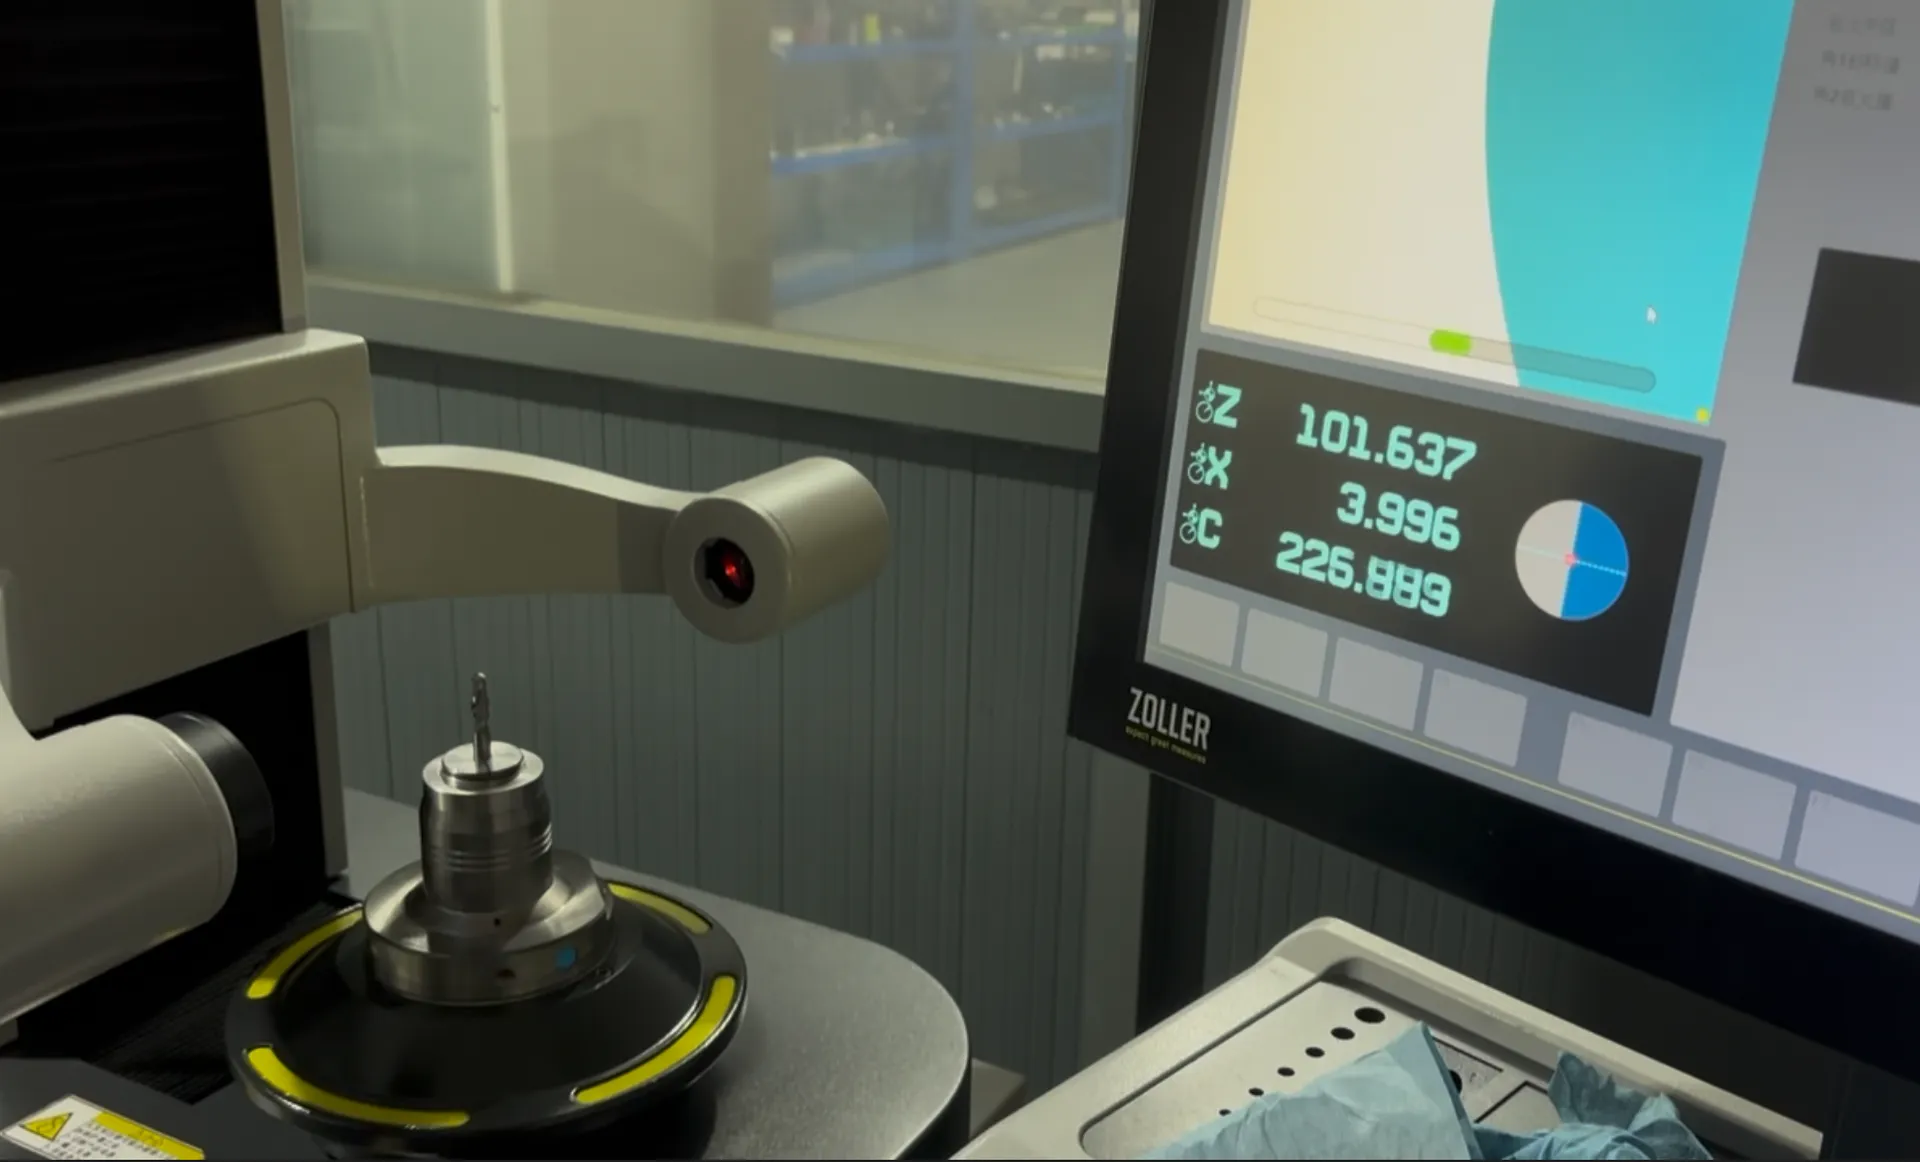
Cutter diameter, end-face geometry, runout, and cutting-edge condition are checked to support accurate slots, walls, and pocket floors. A dimensional report can be supplied with the order for acceptance and traceability.
Square end abrasive-material machining
The 3DEM series uses a square-end geometry for flat pocket floors, slots, shoulders, side walls, and edge milling. Its diamond-coated carbide edge is designed for graphite electrodes and, after application validation, abrasive non-metals such as CFRP and GFRP.
Square ends can machine abrasive composite edges and pockets where a flat floor is required; select entry and support to limit fibre breakout.
Related graphite tooling