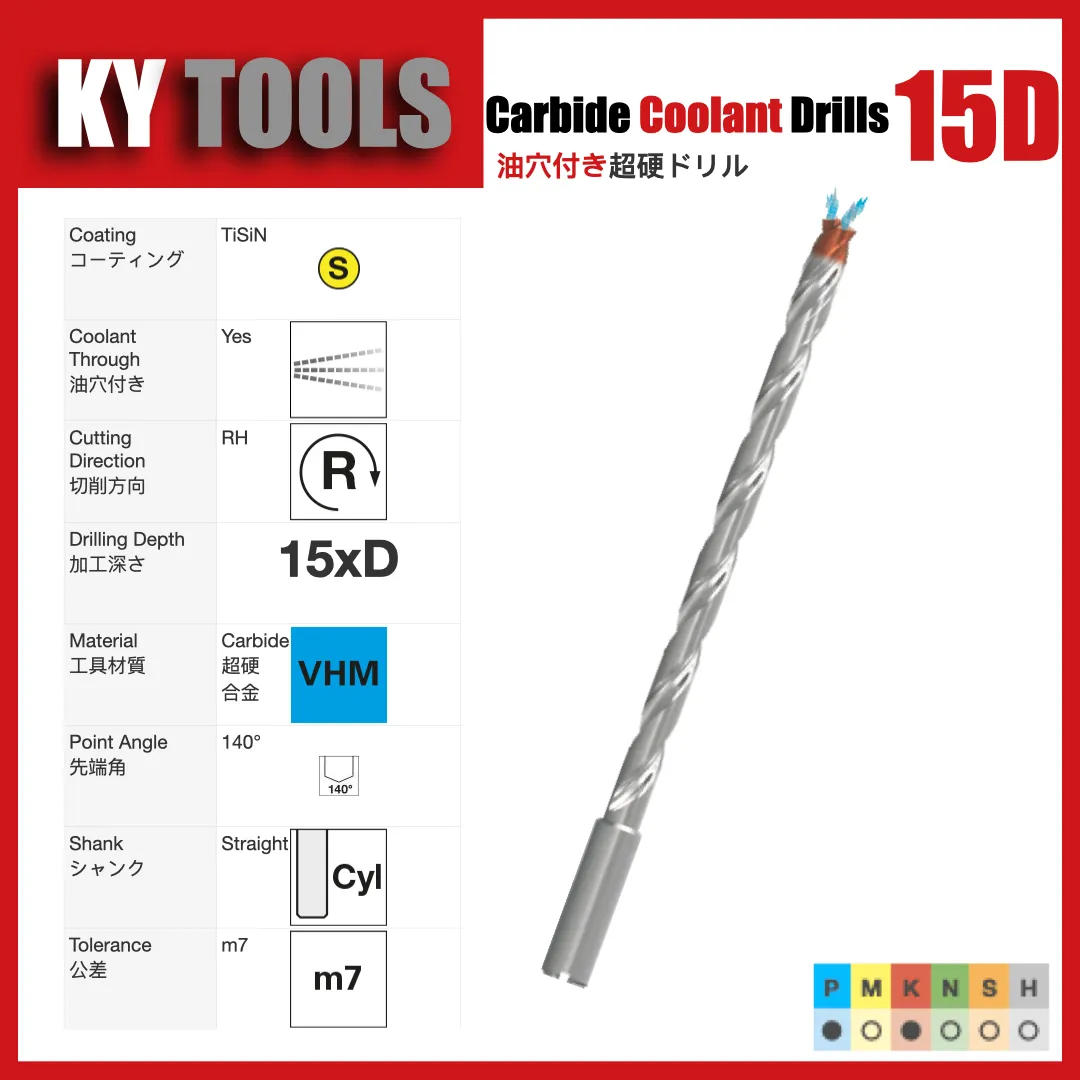
A practical buyer guide for 15D carbide coolant drills: what 3D-25D means, what DIN 6537 defines, current 15D size-price references, and why buyers compare KYTools with European-style coolant drill geometry.
When a buyer searches for Gühring 15D drill price, the real question is broader than one brand: what depth ratio do I need, what DIN 6537 size fits my drawing, what should a reliable 15D coolant-through carbide drill cost, and can I source it with stable quality and shorter lead time? This guide answers those questions from the tooling side.
Useful product pages
Full 15D SKU table with diameter, flute length, shank, overall length, reference price and RFQ entry.
Family page for German standard-size coolant-through carbide drills from 3D through 25D.
Send diameter list, material, coolant pressure, tolerance, coating preference and annual quantity.
What 3D, 5D, 8D, 12D, 15D, 20D and 25D mean
For solid carbide drills, 3D, 5D, 15D and 25D describe the usable hole depth as a multiple of the drill diameter. A 10 mm 15D drill is intended for roughly 150 mm class drilling depth. The higher the D ratio, the more important rigidity, runout, pilot-hole quality, coolant pressure and chip evacuation become.
| Depth ratio | Plain meaning | Typical use | Process note |
|---|---|---|---|
| 3D | Short-hole drill, about 3x diameter depth | Through holes, stable blind holes, high-feed production | Usually the most rigid and easiest to run. |
| 5D | Medium-depth drill, about 5x diameter depth | Hydraulic blocks, flanges, pump housings | Often benefits from reduced feed on entry. |
| 8D | Deep-hole drill, about 8x diameter depth | Steel, stainless, ductile iron, oil/coolant galleries | Pilot hole and internal coolant are strongly recommended. |
| 12D | Extra-deep drill, about 12x diameter depth | Oil galleries, tie-rod holes, forged/cast housings | Pilot hole, rigid holder and coolant pressure become critical. |
| 15D | Ultra-deep drill, about 15x diameter depth | Crankshaft passages, heat-exchanger plates, mould cooling | Runout and coolant flow decide tool life. |
| 20D | Precision deep-hole drill, about 20x diameter depth | Power-generation parts, hardened steel, nickel alloys | Needs controlled entry and high-pressure internal coolant. |
| 25D | Maximum-depth standard range, about 25x diameter depth | Aerospace, mould cooling, medical and long-reach holes | Treat the pilot drill and machine setup as part of the tool system. |
The D ratio is not a marketing label. It tells you how much guidance, coolant pressure and process control the hole will require.
What DIN 6537 means for 15D carbide coolant drills
DIN 6537 is a German standard used for solid carbide twist drill dimensions. For a buyer comparing 15D coolant-through drills, the useful part is dimensional clarity: cutting diameter, flute length, shank diameter and overall length are described in a predictable way.
DIN 6537 helps answer the first purchasing question: does this standard-size drill physically match my hole depth and machine setup? After that, performance depends on geometry, carbide substrate, coating, flute finish, coolant-hole quality and inspection control.
15D DIN 6537 coolant drill sizes and reference prices
The table below lists Solid Carbide Direct / KYTools 15D coolant-through carbide drill reference sizes. Prices are generated from the current site pricing model and may change with raw material, coating, quantity and delivery requirement. For production orders, send the diameter list and annual quantity for a firm RFQ.
| Diameter | Flute L2 | Shank D2 | Overall L1 | Reference price | SKU page |
|---|---|---|---|---|---|
| ø3.00 mm / 0.1181 in | 55.00 mm | 4.00 mm | 95.00 mm | US$18.62 | View SKU |
| ø3.50 mm / 0.1378 in | 55.00 mm | 4.00 mm | 95.00 mm | US$18.62 | View SKU |
| ø4.00 mm / 0.1575 in | 71.00 mm | 4.00 mm | 109.00 mm | US$22.89 | View SKU |
| ø4.50 mm / 0.1772 in | 93.00 mm | 6.00 mm | 133.00 mm | US$40.06 | View SKU |
| ø5.00 mm / 0.1969 in | 105.00 mm | 6.00 mm | 145.00 mm | US$44.37 | View SKU |
| ø5.50 mm / 0.2165 in | 105.00 mm | 6.00 mm | 145.00 mm | US$44.37 | View SKU |
| ø6.00 mm / 0.2362 in | 110.00 mm | 6.00 mm | 148.00 mm | US$45.84 | View SKU |
| ø6.50 mm / 0.2559 in | 120.00 mm | 7.00 mm | 162.00 mm | US$58.36 | View SKU |
| ø7.00 mm / 0.2756 in | 120.00 mm | 8.00 mm | 162.00 mm | US$67.71 | View SKU |
| ø7.50 mm / 0.2953 in | 137.00 mm | 8.00 mm | 180.00 mm | US$75.94 | View SKU |
| ø8.00 mm / 0.3150 in | 137.00 mm | 8.00 mm | 180.00 mm | US$75.94 | View SKU |
| ø8.50 mm / 0.3346 in | 160.00 mm | 10.00 mm | 204.00 mm | US$114.64 | View SKU |
| ø9.00 mm / 0.3543 in | 160.00 mm | 10.00 mm | 204.00 mm | US$114.64 | View SKU |
| ø9.50 mm / 0.3740 in | 175.00 mm | 10.00 mm | 221.00 mm | US$124.52 | View SKU |
| ø10.00 mm / 0.3937 in | 175.00 mm | 10.00 mm | 221.00 mm | US$124.52 | View SKU |
| ø10.50 mm / 0.4134 in | 198.00 mm | 12.00 mm | 247.00 mm | US$179.76 | View SKU |
| ø11.00 mm / 0.4331 in | 198.00 mm | 12.00 mm | 247.00 mm | US$179.76 | View SKU |
| ø11.50 mm / 0.4528 in | 213.00 mm | 12.00 mm | 263.00 mm | US$191.83 | View SKU |
| ø12.00 mm / 0.4724 in | 213.00 mm | 12.00 mm | 263.00 mm | US$191.83 | View SKU |
| ø12.50 mm / 0.4921 in | 248.00 mm | 14.00 mm | 297.00 mm | US$289.55 | View SKU |
| ø13.00 mm / 0.5118 in | 248.00 mm | 14.00 mm | 297.00 mm | US$289.55 | View SKU |
| ø13.50 mm / 0.5315 in | 248.00 mm | 14.00 mm | 297.00 mm | US$289.55 | View SKU |
| ø14.00 mm / 0.5512 in | 248.00 mm | 14.00 mm | 297.00 mm | US$289.55 | View SKU |
| ø14.50 mm / 0.5709 in | 258.00 mm | 16.00 mm | 313.00 mm | US$395.79 | View SKU |
| ø15.00 mm / 0.5906 in | 258.00 mm | 16.00 mm | 313.00 mm | US$395.79 | View SKU |
Reference prices are calculated from the live Solid Carbide Direct / KYTools drill pricing model. Final quote depends on quantity, coating, tolerance, material and delivery schedule.
15D application and process notes
At 15× diameter, this drill enters territory typically reserved for gun drills or BTA deep-hole systems — but at a fraction of the setup complexity. Purpose-engineered for crankshaft oil passages, long tie bolts, and heat-exchanger tube sheets. Full-diameter internal coolant delivery is mandatory.
| Process item | 15D recommendation | Why it matters |
|---|---|---|
| Application fit | Crankshaft oil passages, Long tie bolts, Heat-exchanger plates, Deep mould cooling features | Confirms whether the depth ratio matches the workpiece and production goal. |
| Feed-in method | Use a dedicated pilot hole, low runout holder, and controlled feed-in. Once guided, run steady feed with no dwell. | Entry stability controls runout, chipping and hole straightness. |
| Pilot hole | Required. Pilot hole quality controls entry accuracy and tool life at this depth ratio. | Pilot quality becomes more important as the D ratio increases. |
| Cooling requirement | Internal coolant at 50-70 bar with stable flow is recommended; verify filtration for small diameters. | Internal coolant is what keeps chips moving and temperature under control. |
Gühring-style tool design: what we focus on
- Point geometry: a stable self-centering point reduces entry wander and thrust load before the margins are fully guided.
- Double margin design: two guiding lands support hole straightness and roundness, especially in 15D drilling and longer deep-hole applications.
- Internal coolant channels: coolant reaches the cutting edge directly, helping flush chips before they pack in the flute.
- Polished flute surface: a super-mirror flute finish lowers chip friction and helps prevent chip welding in steel, stainless and ductile iron.
- Controlled edge preparation: the cutting edge must be sharp enough to cut cleanly but protected enough to resist micro-chipping.
- Application-specific coating: TiSiN / Balzers-class PVD coating selection depends on steel, stainless, cast iron or difficult alloy work.
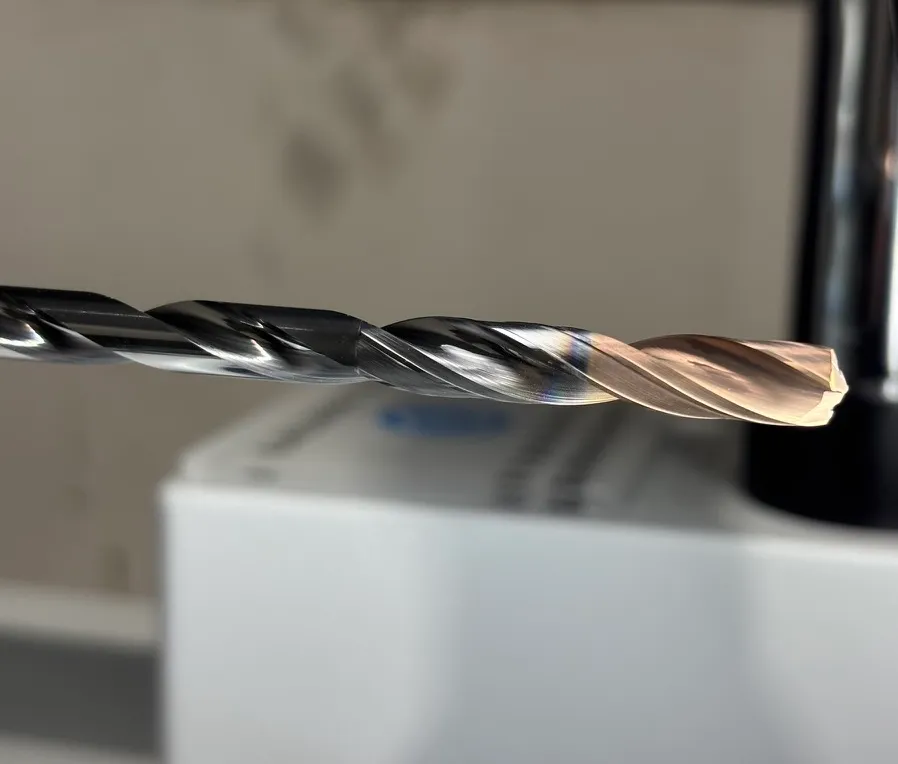
Walter grinding, ZOLLER inspection and super-mirror flutes
The design only matters if it can be repeated. KYTools uses Walter CNC grinding for point geometry, flute profile, margin control and runout consistency. ZOLLER Inspector measurement checks diameter, runout, point angle and margin width before shipment. For 15D coolant drills, flute polishing and coolant-hole quality are especially important because chip evacuation is often the real failure point.
| Capability | What it controls | Buyer benefit |
|---|---|---|
| Walter CNC grinder | Point geometry, flute profile, margin geometry and repeatability | More stable batch-to-batch performance than uncontrolled manual grinding. |
| ZOLLER Inspector | Diameter, runout, point angle, margin width and visual measurement records | Better confidence before tools are shipped into production. |
| Super-mirror flute finish | Chip friction and chip flow through the flute | Less chip packing, less heat and smoother evacuation in 15D holes. |
| Double margin grinding | Guidance lands and hole support | Improved straightness and hole quality in deep drilling. |
| Internal coolant hole quality | Coolant delivery to the cutting zone | More reliable chip flushing and temperature control. |
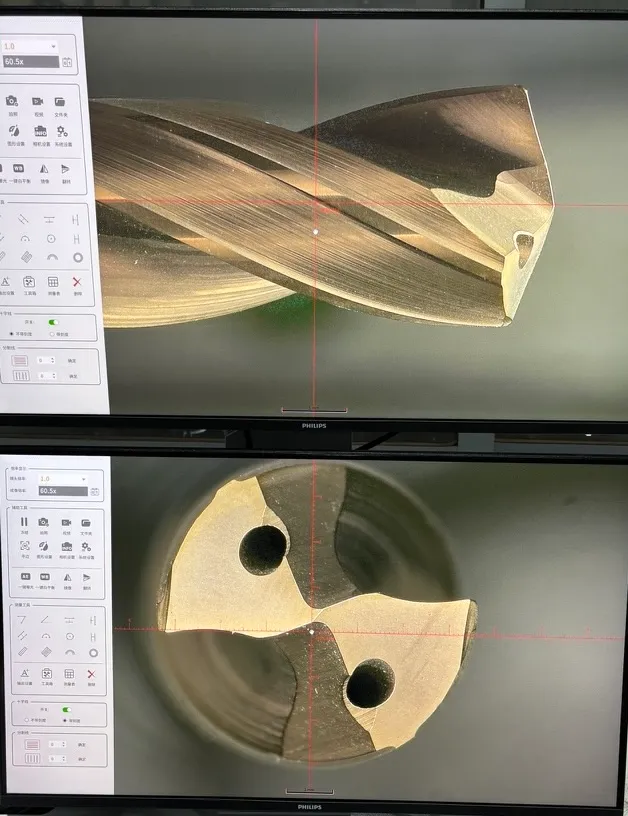
Why choose Solid Carbide Direct / KYTools
- DIN 6537 standard-size range from 3D to 25D for coolant-through carbide drills.
- Factory-direct pricing with visible 15D reference prices and RFQ support for production quantities.
- Gühring-style European geometry logic without asking the buyer to pay distributor layers.
- Double margin, internal coolant, polished flute and coating options for deep-hole applications.
- Walter grinding and ZOLLER inspection for repeatable geometry and measurable quality control.
- MOQ from 1 piece for samples, with 1-15 day lead time for many standard tools.
- Engineering review for material, coolant pressure, pilot hole, holder runout and hole tolerance before production.
What to send for a fast 15D drill RFQ
- Diameter list and quantities, for example 6 mm, 8 mm, 10 mm and 12 mm 15D drills.
- Work material and hardness, such as stainless steel, alloy steel, ductile iron or cast iron.
- Hole depth, blind or through-hole condition, tolerance and surface finish requirement.
- Machine model, toolholder, runout condition, coolant pressure and filtration quality.
- Current tool brand/code if you are comparing with Gühring, Walter, Sandvik or another European supplier.
- Required lead time, sample quantity and annual production quantity.
Next pages for RFQ and comparison
Open the live 15D DIN 6537 product table with SKU links and current reference prices.
Compare 3D, 5D, 8D, 12D, 15D, 20D and 25D coolant-through drill families.
Send drawing, material, diameter list, coolant pressure, coating and annual quantity.
标签